The Handover Between Operations: Auditing Datum Continuity in Multi-Setup Precision Work
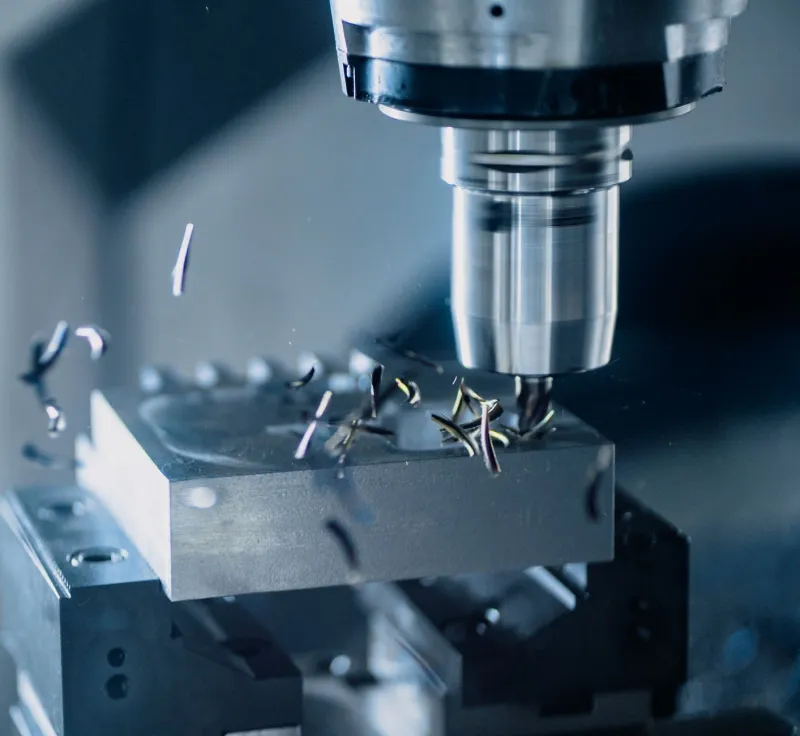
A precision component can leave the first machine within tolerance and still carry avoidable risk. The danger is not always the first cut. It is the handover to the next operation, where the reference frame established in one setup must be reproduced in another. For UK buyers reviewing 2026 supply plans, that handover deserves the same scrutiny as material certification or final inspection.
Re-datuming is often treated as a workshop detail. In practice, it is a quality decision hidden inside the process route. The drawing may define datums clearly, but the supplier must realise those datums through fixtures, clamping, probing and inspection. Each transfer introduces a new opportunity for drift, stack-up error or interpretation. The buyer does not need to dictate the method, but the buyer should understand how the promise of continuity will be proved.
The second operation is where the reference frame can move
A drawing datum is a theoretical reference. A machined part is a physical object with burrs, residual stress, clamp marks and surface variation. When a part is moved from one setup to another, the surfaces used for location may not be the same surfaces that final inspection will use. If an intermediate datum is introduced, the supplier is making a translation between the drawing requirement and the manufacturing process. That translation is legitimate, but it needs control.
Consider a housing that is faced and bored in the first operation, then drilled and milled from a second side. The second operation may locate on the first machined face. If that face has slight distortion after clamping, or if a chip is trapped at a fixture contact, the second operation can be perfectly executed in relation to a reference frame that has already shifted. Final inspection may still pass if tolerances are wide enough. If they are not, the problem appears late and is difficult to attribute.
Fixture strategy is part of the quality record
Buyers should not expect to approve every fixture design. They should, however, expect a coherent account of how the part is located at each stage. A useful question is simple: which surfaces locate the part in each operation, and how do those surfaces map to the drawing datums? If the answer is vague, the process route may be relying on operator skill rather than controlled method.
Fixture choice also affects repeatability. Dedicated fixtures, soft jaws, tombstones and modular systems can all be appropriate. What matters is whether the fixture controls the required degrees of freedom, whether loading is repeatable, and whether contact points are protected from swarf and damage. A fixture that works for one part may not remain capable across a batch. Wear, cleanliness and maintenance are not administrative matters; they are part of datum continuity.
Continuity needs evidence, not assurance
A supplier may state that the second operation uses the same datums as the drawing. That statement is a claim. The buyer should ask what evidence supports it. Depending on the component and criticality, useful evidence can include a setup sheet showing datum references and fixture identification, a first-off inspection at each operation, probe or CMM alignment reports, and a signed route card that records the transfer between operations.
In-process verification is particularly important. If a feature produced in the first operation is used to locate the second, the supplier should check that feature before production continues. That check need not be exhaustive. It should be targeted at the datum relationship that matters. If the first operation is close to a tolerance limit, the second operation may amplify the problem. A controlled process will define what happens in that situation rather than discovering it at final inspection.
Questions to put in the enquiry
For a multi-setup part, the following questions can be included in the enquiry or quality schedule without implying distrust. They simply make the handover visible.
- Which surfaces locate the component in each operation, and how are they related to the drawing datums?
- If intermediate datums are used, who approves the translation and how is the tolerance stack verified?
- What first-off inspection is performed at each setup before production proceeds?
- What in-process checks confirm datum continuity after the part is transferred?
- How are fixture wear, swarf, burr and clamping distortion controlled between operations?
- What records will accompany the inspection pack to show the sequence of setups and checks?
- How are deviations handled if the second operation reveals alignment drift?
- Can the supplier provide a redacted route card or setup sheet for a comparable part?
- How is the fixture itself verified, maintained and identified for traceability?
These questions are not a substitute for supplier expertise. They are a way for the buyer to confirm that expertise is documented. A supplier who can answer them clearly is usually a supplier who has already thought about the risk.
What good sign-off looks like
At sign-off, the buyer should expect more than a final dimensional report. The report confirms the result; it does not necessarily explain the process. A stronger pack includes the route card, operation numbers, datum references, fixture identification and first-off results at each setup. For critical features, a CMM alignment report can show how the inspection reference frame was established. The buyer does not need every dimension, but the buyer does need confidence that the reference frame was controlled from the first cut to the last.
Re-datuming is a promise that the second operation will respect the first. Like any promise in precision manufacturing, it should be proved. UK buyers who ask about fixture strategy, in-process verification and handover evidence are not adding bureaucracy. They are protecting the tolerance that the drawing already requires.