Who Is Holding the Micrometer? Measurement Capability as a Contract Term
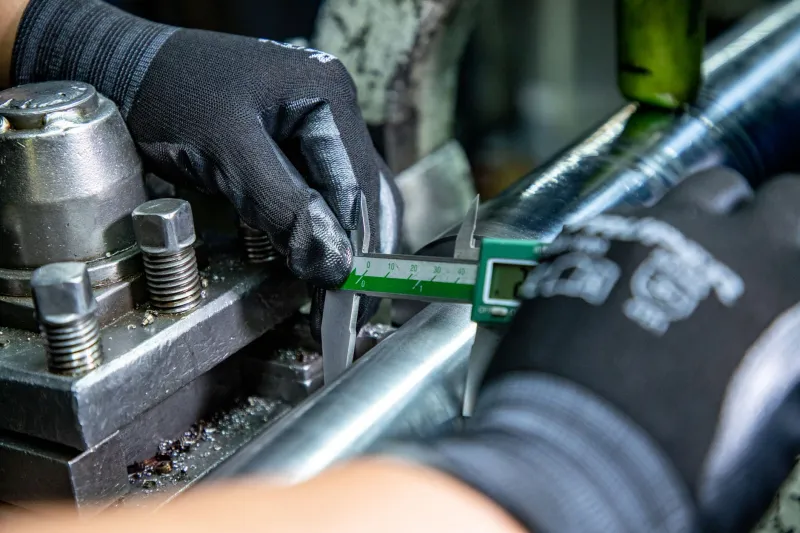
A calibration certificate is often treated as the end of a measurement argument. It is not. It is a record that an instrument was compared with a reference under controlled conditions, usually in a laboratory. It says little about whether the same instrument, in a workshop, on a production part, in the hands of a particular operator, can reliably distinguish a good component from a marginal one. That distinction matters most when a purchase order depends on a dimensional report.
For UK buyers of precision parts, the practical question is not whether the supplier owns a calibrated micrometer. It is whether the measurement system behind the inspection report is capable of the tolerance being claimed. Calibration and capability are related, but they are not interchangeable. Confusing them is one of the quieter ways a supply relationship goes wrong.
Calibration answers a narrower question
Calibration establishes traceability. It checks an instrument against a reference that can be linked to national standards, and it identifies bias at defined points. A UKAS-accredited calibration certificate is a useful document, and in many supply chains it is a mandatory one. But it does not account for the fixture that holds the part, the operator who applies the gauge, the temperature of the workshop, the cleanliness of the surface, or the way the reading is recorded.
Measurement capability looks at the whole system. It asks whether repeated measurements of the same characteristic, under normal production conditions, produce results that are close enough together and close enough to the true value to support an accept or reject decision. A calibrated gauge can still fail that test.
Consider a shaft diameter specified at 25.000 mm plus or minus 0.010 mm. A micrometer with 0.001 mm resolution looks adequate on paper. If its repeatability and operator reproducibility together consume 0.006 mm of the tolerance, the measurement system is already using a large share of the available band. A gauge R&R study might show a percentage of tolerance in the region of 30 per cent. At the limits, the inspection report begins to resemble a coin toss. The three decimal places on the certificate create a confidence the method has not earned.
When the gauge agrees with itself, but not with the next operator
Gauge R&R separates two sources of variation. Repeatability is the variation seen when one operator measures the same part several times with the same gauge. Reproducibility is the variation seen when different operators measure the same parts with the same gauge. A gauge can be repeatable in one pair of hands and still produce different results in another. Clamping force, orientation, hand warmth, cleaning routine and the order in which readings are taken can all shift the result.
This is why a dimensional report signed by one inspector is not evidence of a capable system. It is evidence of one operator on one day. If that operator is unusually careful, the buyer may be reassured by a capability that does not exist across the production team. If the operator is less careful, good parts may be rejected. A marginal gauge can also make bad parts look acceptable when bias runs in the favourable direction. In a dispute, both parties may hold calibration certificates and still disagree about the part, because they never agreed the measurement method.
What a gauge R&R study should show
A conventional measurement systems analysis uses production-representative parts spanning the process variation, several operators and repeated trials in randomised order. The output usually includes the percentage of tolerance consumed by gauge variation and the number of distinct categories the system can resolve. Common acceptance bands are under 10 per cent as acceptable, 10 to 30 per cent as conditional, and above 30 per cent as unacceptable. Those bands are not universal law. A safety-critical feature and a non-critical clearance may justify different thresholds, but the threshold should be agreed before the order, not argued after a rejection.
The study should be relevant to the characteristic. A gauge R&R performed on a clean, polished reference block is not the same as one performed on a production part with the specified surface finish and fixturing. The operators should be representative of those who will inspect the work. The gauge should be identified, and its calibration status should be current. The raw data should exist, not merely a one-page summary.
Purchase-order wording that puts capability on the record
A purchase order does not need to become a metrology manual, but it should make the measurement method a contractual matter. The following clauses are a practical starting point for UK precision supply.
- Measurement method schedule. The Supplier shall measure the characteristics listed in Schedule X using the gauge type, resolution, fixturing, reference temperature, cleaning procedure and number of readings stated in that schedule. No substitution shall be made without the Buyer's written approval.
- Gauge R&R evidence. For each characteristic marked capability-critical, or with a tolerance of 0.05 mm or less, the Supplier shall provide a gauge R&R study not more than 12 months old. The study shall use production-representative parts, at least three operators and three trials. The percentage of tolerance consumed by gauge variation shall not exceed 10 per cent unless a different limit is agreed in writing. Results between 10 and 30 per cent shall require a documented guard band and Buyer approval. Results above 30 per cent shall not be accepted for final inspection without rework of the measurement method.
- Operator variation. The study shall identify the operators and include evidence that they are trained for the method. If the inspection operator changes, the Supplier shall notify the Buyer and revalidate where the characteristic is capability-critical.
- Decision rules. Acceptance shall be based on a declared decision rule consistent with ISO 14253-1, including the expanded measurement uncertainty for each characteristic. The Supplier shall state the uncertainty rather than implying that the reported value is exact.
- Evidence and access. Raw study data, gauge identification and calibration certificates shall be retained and made available to the Buyer on request. A summary sheet without the underlying readings is not sufficient evidence.
- Change control. Any change to the gauge, fixture, measurement software, inspection sequence or environment shall trigger revalidation before the next shipment.
- Independent review. Where a dispute arises, either party may appoint an independent UKAS-accredited laboratory to measure the parts. The agreed method schedule should be used as the basis for that review.
Match the rigour to the characteristic
There is a commercial risk in over-specifying measurement capability. A buyer who demands a full gauge R&R study for every dimension on every drawing will add cost and may encourage paper compliance rather than genuine control. The sensible approach is risk-based. Critical-to-function features, mating interfaces, safety-related characteristics and regulated dimensions deserve strong evidence. Non-critical reference dimensions may need only a calibrated gauge and a simple repeatability check.
The decision should be conscious and recorded. UK precision suppliers range from large, well-resourced firms to small workshops with deep technical skill but limited metrology administration. A clause that is impossible to meet will narrow the supply base unnecessarily. A clause that is clear, proportionate and agreed at enquiry will do the opposite.
The certificate is a starting point
A calibration certificate proves that a gauge was checked. It does not prove that the measurement is fit for the purchase order. For buyers, the useful move is to treat measurement capability as part of the specification, alongside material, finish and delivery. Ask for gauge R&R evidence before the first delivery. Agree the method, the operators and the acceptance criteria while there is still time to change them. A dimensional report is only as strong as the measurement system behind it, and that system should be visible before the part is accepted.